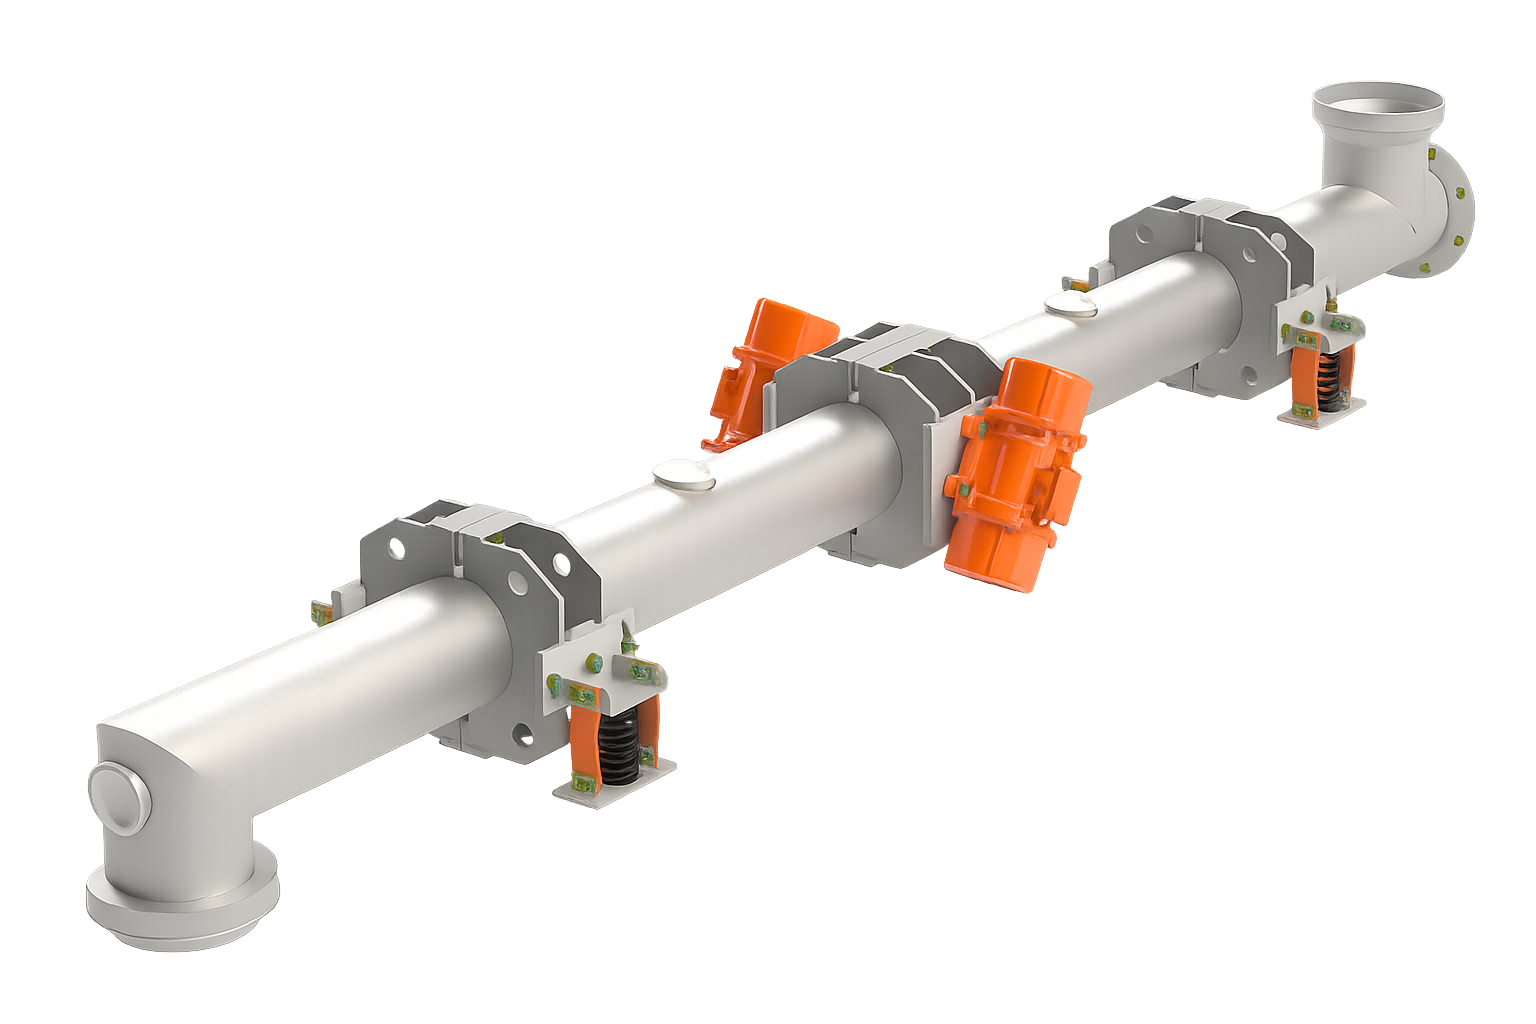
Conveyors
Our industrial tube conveyors offer a completely enclosed, dust-tight transport solution that seals your materials safely inside, eliminating environmental contamination and product loss. Engineered to handle delicate materials, fine powders, or hazardous chemicals, these systems move bulk goods smoothly without the degradation or separation caused by traditional open belts. The flexible, compact design lets you reroute materials around existing equipment without wasting valuable floor space. If you need a clean, safe, and reliable way to move material from point A to point B, our tube conveyors are built to perform.
Typical applications
- Conveying materials from one process to another.
- Delivery of material onto separation equipment.
- Discharging materials from storage hoppers/silos.
Design Options
- Fabricated from mild steel or stainless steel (304 or 316).
- Enclosed design.
- Fixed or variable speed drive control panels.
- High temperature and ATEX designs.
- Covers and seals for dust tight operation.
- Multiple inlet and outlet configurations.
- Adjustable or fixed angle spring brackets.
- Available with electric or pneumatic drives.
- Diameters up to 600mm and 10m long. Configurable for multiple units. to extend the conveying length.